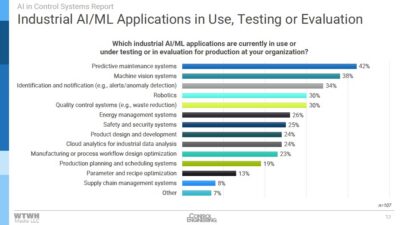
Answers are available for using modern machine vision tools enabled by artificial intelligence (AI), as explained in an SPS Atlanta presentation. See AI machine vision applications and examples.

AI-enabled machine vision insights
- Machine vision-enabled with artificial intelligence is available for industrial use.
- AI visual inspection applications and industries are many.
- Challenges and cures for machine vision applications can be helped in part by AI-enabled machine vision that uses integrated machine vision AI engines.
Why aren’t industrial AI-enabled machine vision systems more widely used? What applications are appropriate for machine vision? How can artificial intelligence (AI) be applied more easily? These were among questions answered Jim Wilmot, portfolio sales enablement manager at Siemens Digital Industry, in the presentation “AI-powered visual quality inspection,” at SPS Atlanta 2025. His topics included industrial AI and machine vision (ML), AI visual quality inspection and related technologies, basic and advanced.
Why now for AI-enabled machine vision?
Wilmot said manufacturers are struggling with AI and survey data shows it with 40% thinking AI is not trustworthy, 92% answering they lack AI-skilled experts and 16% saying they are not achieving AI-related goals.
“Why is industrial AI machine vision and why now?” Wilmot asked. “The answer isn’t: ‘Because I took AI class in college.’”
Now is a good time to apply AI because of machine vision’s use of AI has advanced along with the growing ecosystem enabling machine-vision applications. These include more capable sensors, hardware, software, industrial PCs (IPCs), AI-powered chipsets, more easily connected edge devices, gateways, high-powered programmable logic controller (PLCs) with built-in networks, integrated diagnostics, security and safety and flexible high-level programming. Smart field devices use GigE and improved USB communications, 3D cameras and compact sensors with remote connectivity. Better automation infrastructure eases connectivity from devices to the cloud, enabling digitalization and smart manufacturing. Wilmot emphasized that AI is enhancing control; programmable logic controllers (PLCs) are not going away.
AI visual inspection applications listed
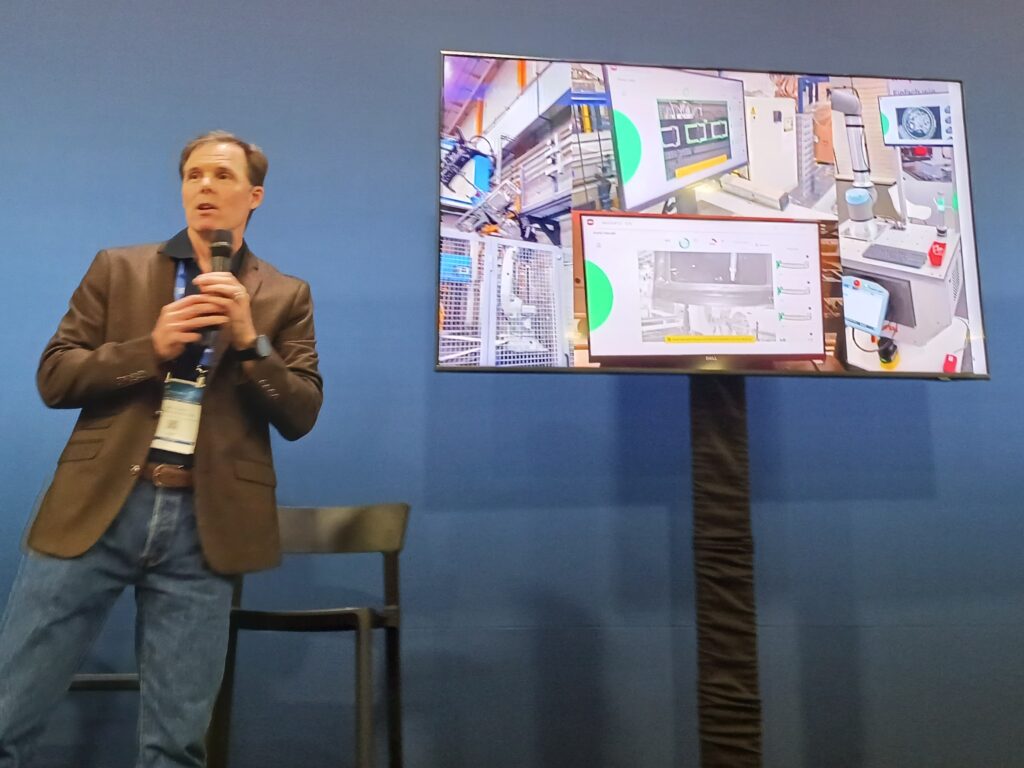
More than 70% of the current AI opportunities in the pipeline are vision use cases. Applications are many for AI-enabled machine vision (Figure 1), but the four big areas for AI visual quality inspection are: Defect detection (scratches, dents, discoloration), surface inspection (uniformity, consistency, especially important for electronics and pharmaceuticals), assembly verification (screws, labels, part alignment) and presence and/or object detection (components, features). A diverse range of parts and industries are within the latest AI-enabled machine vision technology capabilities (Figures 2 and 3).
Technology solutions for machine vision applications can overlap with vision sensors, smart cameras, and custom vision systems in the mix. Often the cheapest solution can be the best, Wilmot said.
Hardware and software can be bundled to ease implementation.
Challenges, cures for AI-enabled machine vision
Challenges in machine vision applications can include changing light conditions, parts and products in various positions in production, changes in production lines and locations, variation in defect sizes and materials, often small defects and miniature component assembly.

Attributes desirable in a machine vision system to address those challenges may include:
- Industrial grade designs
- Scalability
- Easy setup
- Easy use for different applications
- AI advantages without AI expertise
- Easy user interface to guide the user
- Small sample size for use (such as 20 good samples and no defective ones)
- Self-adaptive capabilities that can recognize unforeseen defects and surface variations typical in many industries.

Courtesy: Mark T. Hoske, Control Engineering
Integrated machine vision AI engines
AI engines (algorithms) can focus on various tasks, such as image acquisition, part recognition and part inspection (Figure 4). AI enhancements help more affordable machine vision offerings quickly work through challenges, such as finding debris in a field of vision with reflections, for instance.
The graphical user interface should include ease of use and automated mark-up, guides to help the user succeed in the application and integrate support, Wilmot added.

Figure 5 shows Siemens machine vision products, and Figure 6 shows a machine vision application demonstrated in the Siemens SPS Atlanta 2025 booth.
Mark T. Hoske is editor-in-chief, Control Engineering, WTWH Media, [email protected].
Keywords
Machine vision, industrial AI for vision
Consider This
Are your machine vision technologies intelligent enough to make your job easier?
You also might like
Learn more about Siemens AI-enabled machine vision.
https://www.siemens.com/global/en/products/automation/topic-areas/industrial-ai/inspekto.html
Control Engineering has more machine vision information.
https://www.controleng.com/mechatronics/vision-and-discrete-sensors
Control Engineering has more on AI and machine learning.